Industry case
Applications
New energy industry
Release time:
2025-02-28
I. Project Overview
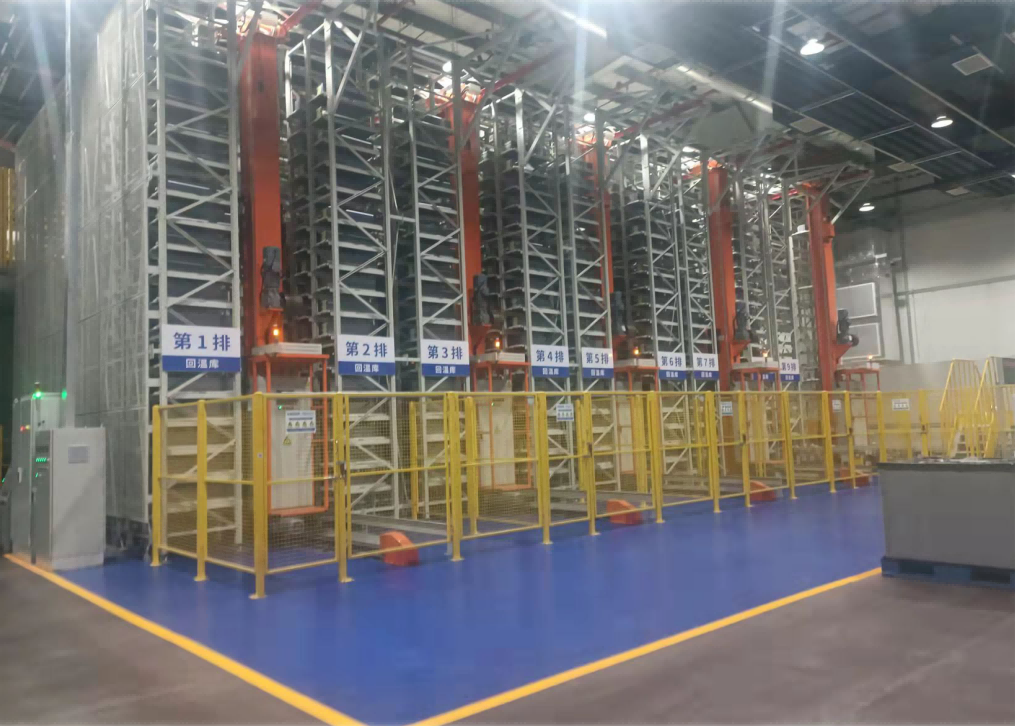
A certain company, based in the photovoltaic and semiconductor industries, is dedicated to the research and development, and large-scale manufacturing of high-end equipment in the field of intelligent manufacturing. The project covers an area of nearly 3500 square meters and includes 2 finished product warehouses, 2 line-side warehouses, 1 raw material tank warehouse, and 1 single-crystal warehouse. The number of storage locations are as follows:
- Finished product warehouse: 3272 storage locations
- Line-side warehouse: 576 storage locations
- Raw material tank warehouse: 2860 storage locations
- Single-crystal warehouse: 2090 storage locations
It uses intelligent logistics equipment such as stacker cranes, high-bay racking, chain conveyors, RGV, packaging machines, and lifts. The single pallet cargo weighs 2000kg with dimensions of 1200X1200X1750mm, and the equipment has a net height of 8.2m.
II. Key Technologies
- Intelligent Equipment Integration:
- Twin-aisle stacker crane: Modular lightweight design, supporting dual closed-loop PID control and an S-shaped speed curve, ensuring stable operation and convenient maintenance.
- RGV conveyor collaborative operation: High operating speed, smooth acceleration and deceleration, measures to prevent derailment. Emergency stop function to ensure safety during maintenance. Abnormal cargo position detection function to prevent failures caused by cargo deviation from the center during transfer. Safety devices include safety railings, safety gates, and safety switches.
- Digital Twin Management: Real-time inventory monitoring based on the WMS+WCS system, achieving full process material tracking and seamless integration with the MES system.
- Efficient Logistics Management: Cross-area linkage, connecting different factory warehouse areas through reciprocating lifts, dynamically balancing material distribution, and improving turnover efficiency.
- Environmental Adaptability: Uses high-temperature resistant and anti-corrosion materials and is equipped with an intelligent temperature control system to ensure the safe storage of new energy materials.
III. Economic Benefits
- Cost Savings:
- Labor costs: Reduces manual picking personnel by 80%, saving over 2.76 million yuan annually.
- Equipment maintenance: Automated equipment reduces the procurement and maintenance costs of traditional forklifts, saving a total of over 1 million yuan.
- Efficiency Improvement:
- Storage capacity: Space utilization rate increased to 90%, warehouse capacity increased 5 times compared to traditional flat warehouses.
- Operation speed: The inbound and outbound composite cycle efficiency reaches 140 pallets/hour, and the logistics cycle is shortened by nearly half.

Previous Page
Next Page
Customer Service Hotline
E-mail:wuzp_2008@sina.com
Address: No.1, Guangming Road, Huo Pai Industrial Park, Xiangzhou District, Xiangyang City
 WeChat
This website already supports IPV4 / IPV6 bidirectional access
Copyright © 2024 KEDE ZHINENG ALL RIGHTS RESERVED.