Industry case
Applications

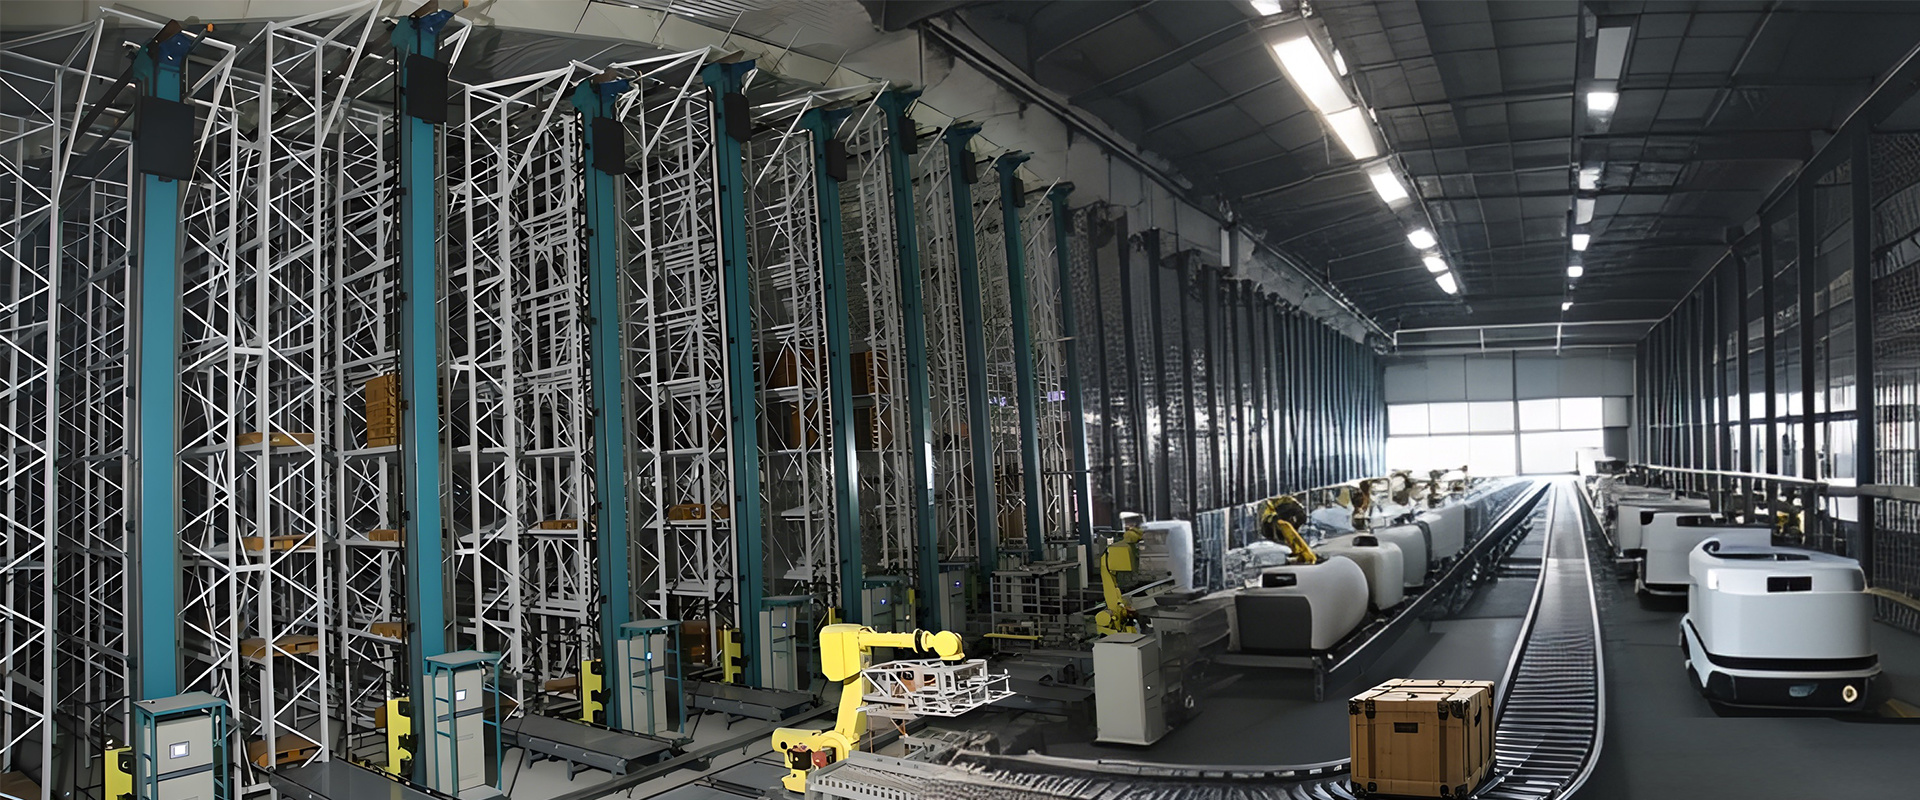
KEDLE SMART built an intelligent automated warehouse for a large chemical company, addressing issues such as low efficiency, high labor costs, and significant safety hazards in traditional warehousing. The project utilizes an automated high-bay warehouse system to achieve intelligent management of the entire packaging, warehousing, and outbound process. It is suitable for storing Class C solid materials (such as lubricating oil and butyl/pentyl chemicals).
DetailsCustomer Service Hotline
E-mail:wuzp_2008@sina.com
Address: No.1, Guangming Road, Huo Pai Industrial Park, Xiangzhou District, Xiangyang City
WeChat
This website already supports IPV4 / IPV6 bidirectional access
Copyright © 2024 KEDE ZHINENG ALL RIGHTS RESERVED.